
Application of technology in sand production wells Hydraulic pump system Application of technology in scaling wells Application of technology in corrosive wells Technical application in high-temperature wells Application of technology in water injection wells Application of technology in heavy oil wells Technical requirements in oil wells with unstable production capacity Small diameter electric pump set Intelligent Control System for Submersible Electric Pump |
Supporting process technology for sand production wells:
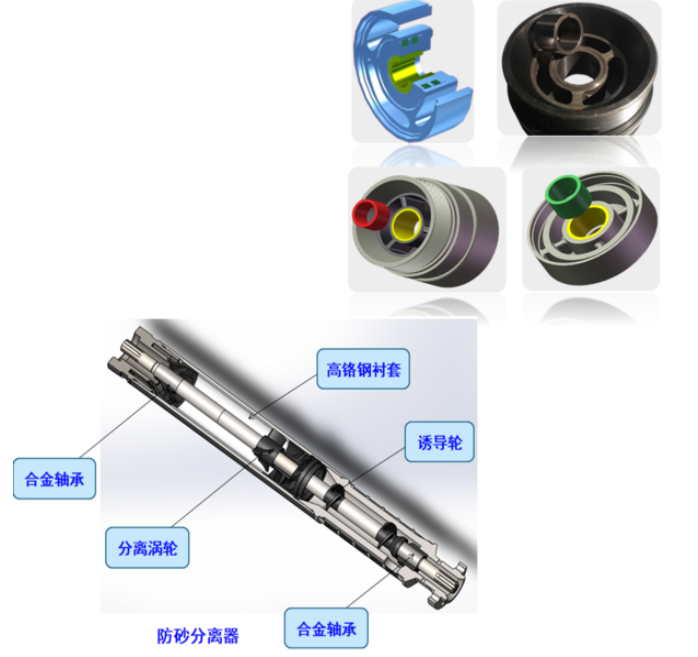
The centrifugal pump and separator are designed with a high hardness and sand resistant structure
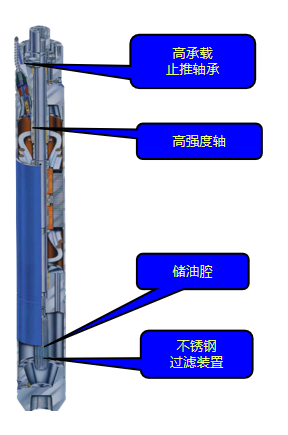
Full compression structure centrifugal pump with high load-bearing thrust protector
Supporting sand filter tube oil production process
Electric pump cover matched with sand filter tube
Leather bowl packer matched with sand filter tube
Technical conditions:
Maximum sand content: ≤ 5 ‰
Sand particle diameter:<0.1mm
Advantages:
Reduce radial wear
Reduce unit vibration
Improve the lifespan of the unit
Reduce operating costs
Features:
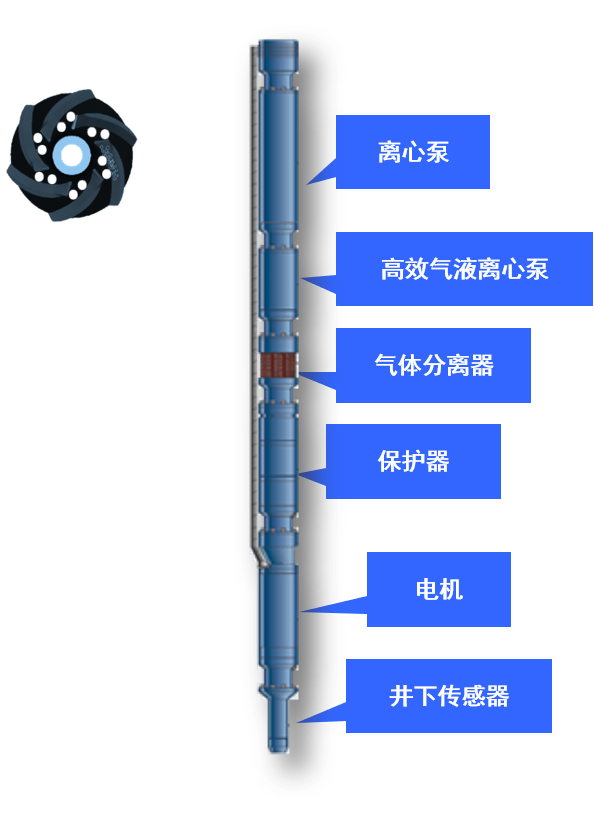
Efficient gas-liquid centrifugal pump
The specially designed pump stage breaks the gas and mixes it evenly with the well fluid
High strength, sand resistant design
Technical conditions:
Free gas content in the pump (with separator):<75%
Free gas content in the pump (used separately):<60%
Advantages:
Eliminate the influence of gas and release the gas lock
Reduce bottomhole pressure
Improve the production of high gas content oil wells
Maintain efficient operation of the pump in a mixed state of oil and gas
High wear resistance
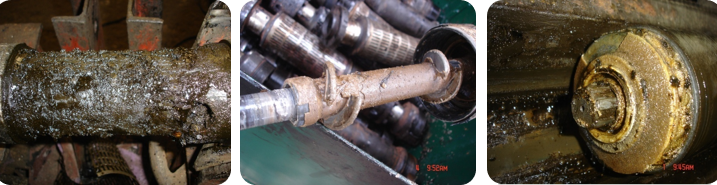
At present, the mature anti scaling technologies applied in submersible electric pump systems mainly include the following:
Surface treatment anti scaling
Chemical scale prevention
Metal anti scaling device
1. Technical application in scaling wells - surface treatment for scale prevention
Surface treatment anti scaling:
By contacting the inner and outer surfaces of the submersible electric pump system with the well fluid, as well as the centrifugal pump guide
The surface of the impeller channel is coated with a thermal spray polymer composite material to prevent scaling.
Technical conditions:
Maximum mineralization degree: ≤ 30000mg/L
Advantages:
Improve operational lifespan
Reduce operating costs
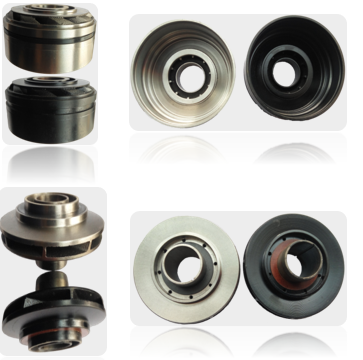
Comparison of guide vanes before and after coating:
2. Technical application in scaling wells - chemical scaling prevention
Chemical scaling prevention:
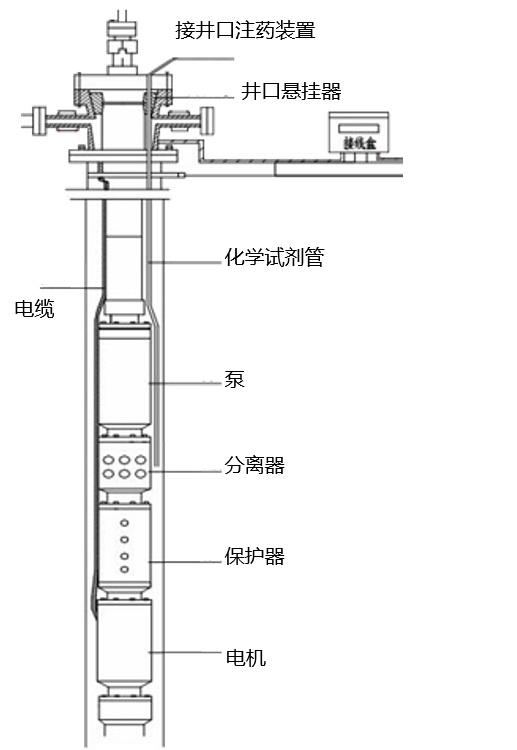
Chemical scaling prevention is a solution to the problem of oil well scaling by adding chemical scaling inhibitors into the production well. The dosing system mainly has the following two solutions:
Option 1:
Pass the injection tube through the wellhead hanger and lower it into the depth of the electric pump unit pump hanger (see left figure). Add scale inhibitor to the well fluid through the chemical reagent tube to solve the problem of oil well scaling.
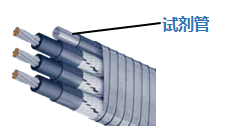
Option 2:
Without changing the conventional process, the structure of the existing flat cable will not be modified. Only during the armor process, the cable and the chemical reagent tube will be armored together.
3. Technical application in scaling wells - metal scale inhibitor
Metal anti scaling device:
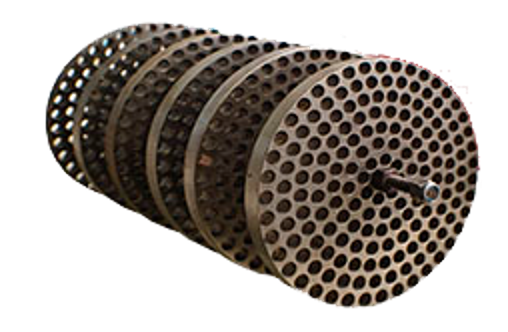
The core of the metal anti scaling device consists of multiple designed orifice plate chips arranged axially in the inner cylinder of the anti scaling device. The fluid enters the inner cylinder of the scale inhibitor through the inlet. The design of the tool ensures that the fluid passing through is in full contact with the surface of the chip's orifice plate. At the same time as the fluid comes into contact with the chip, the chip will cause a polarization effect on the fluid, preventing minerals in the solution from solidifying and settling on the pipe wall or other surfaces downstream of the tool.
Working principle: The core material of the metal scale inhibitor is an alloy material containing various different metal components such as copper, zinc, nickel, etc. The electronegativity of the elements contained in the alloy is lower than that of the ions in the liquid phase. The alloy acts as an electrochemical catalyst, causing the fluid to produce polarization effect, thereby suspending the wax and colloidal substances in the crude oil and preventing them from accumulating and adsorbing on the pipe wall; Make it difficult for various particles and impurities in the liquid phase to combine with each other and form scale.
Surface coating anti-corrosion:
Supersonic spraying of Monel alloy on the surface of the entire machine
Low cost, suitable for general corrosive oil wells.
Stainless steel unit:
Head seat large items: 1Cr13, 2Cr13, 304, etc
Shell: 9Cr1Mo, 316L
Customizable according to user needs
High cost, suitable for severely corrosive oil wells.
Advantages:
Improve the operational lifespan of the unit in corroded wells
Technical conditions:
Oil well temperature: ≤ 204 ° C
Features:
High temperature resistant insulation system
Process technology for improving insulation performance
Specially designed cooling system
Maximum temperature resistance level: 204 ° C
Advantages:
Improve the operational lifespan in high-temperature wells
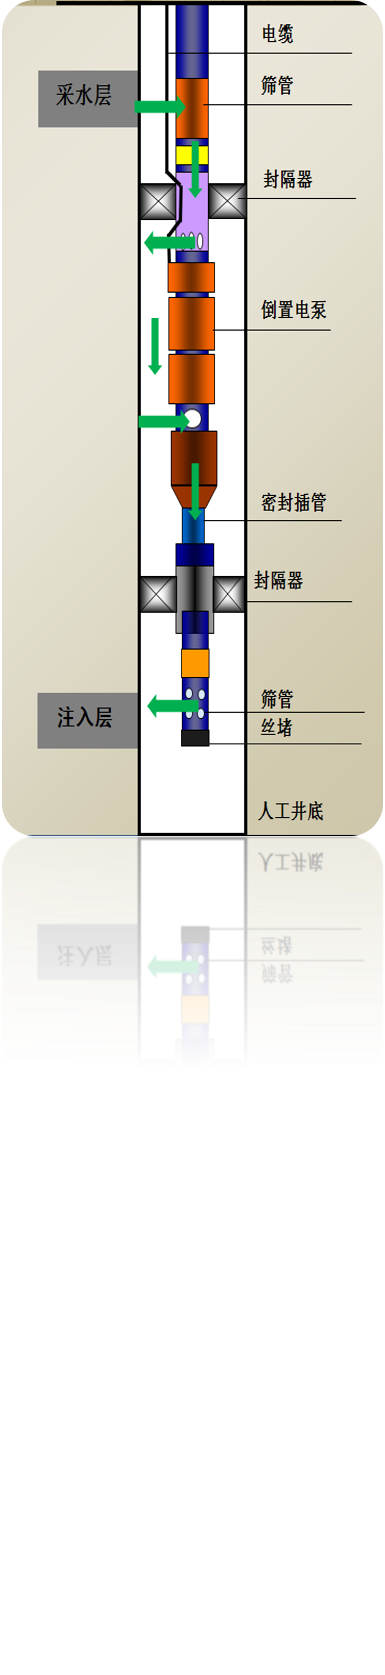
Inverted electric pump unit for same well injection and production
Scope of application:
Remote areas, small fault block oil reservoirs far away from the main blocks, and imperfect injection production well networks, long-term
A block where depressurization mining results in ineffective replenishment of geological energy.
Technical Specifications:
Water injection volume: 30-300m3/d
Increase injection pressure: 5-40MPa
Applicable casing types: 5 1/2 ", 7"
Advantages:
Simple operation and maintenance
No noise, no leakage
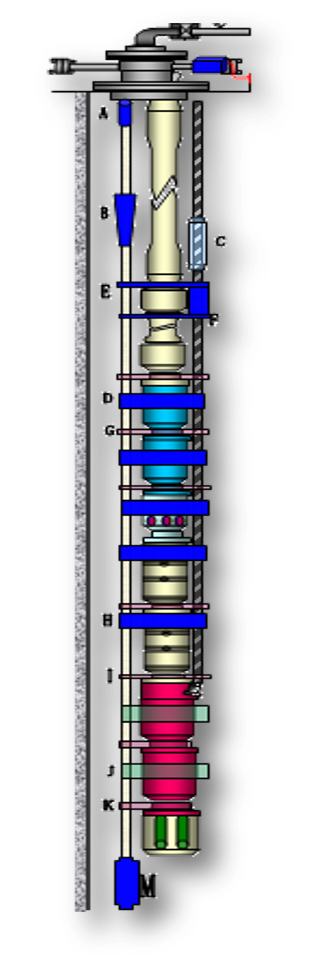
1. Dilution process technology for adding naphtha (or thin oil) to the bypass pipe of the submersible electric pump
Application:
Adapt to well fluid viscosity ≤ 5000mPa · s
Advantages:
The dilution system process of injecting naphtha (or light oil) is beneficial for the recovery of self spraying in oil wells or the
realization of mechanical oil recovery by submersible electric pumps.
Features:
The process technology of using a submersible electric pump to inject naphtha (or thin oil) dilution system is to inject thin oil
into the oil well through a pipeline
(side pipe), so that the thin oil and the heavy oil produced in the formation are fully mixed, thereby reducing the viscosity and
flow resistance of the heavy oil,
increasing the production pressure difference at the bottom of the well, and enabling the oil well to resume self spraying or
achieve mechanical oil recovery by
submersible electric pump.
Engineering case:
Since 2004, nearly 60 oil wells in eastern Venezuela have successfully applied the technology of diluting heavy oil production by
adding naphtha, with an average pump inspection cycle of nearly 1200 days.
In 2009, this injection system was successfully applied in the Shenyang Oil Production Plant of Liaohe Oilfield to solve the problem
of uneven dilution of the ring
sleeve. The average pump inspection cycle of the electric pump was increased from 150 days to 408 days.
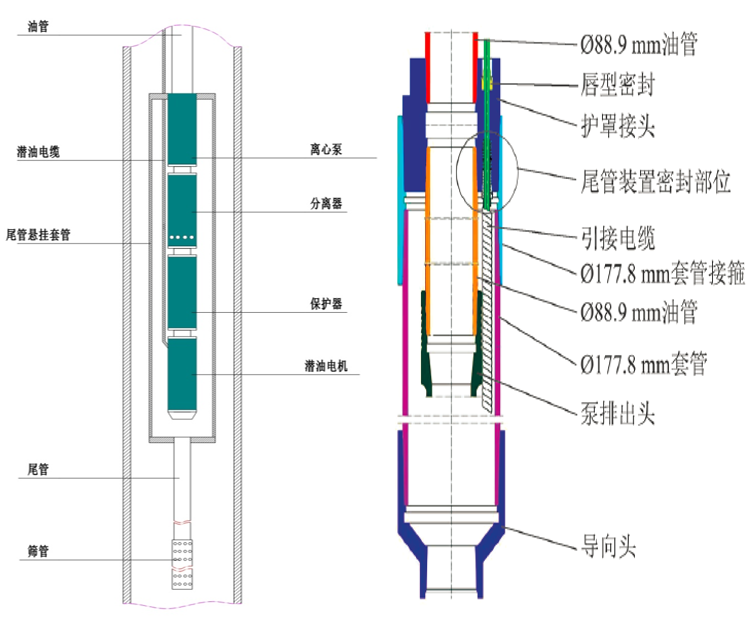
2. Thin oil blending technology for shield submersible electric pump units
The shield of the submersible electric pump unit with a shield is an isolation cover added between the outside of the unit and the
casing to change the entry point of the well fluid, force the well fluid to pass through the outer surface of the motor, and increase the flow rate of the well fluid on the
outer surface of the motor.
Features:
In low yield heavy oil wells, in order to reduce the viscosity of crude oil, viscosity reducers, thin oil or water are usually injected from
the wellhead. Due to the protective
cover, the injected fluid needs to be sucked in from the tail of the oil pipe connected under the cover, thereby increasing the mixing
time and space of thin oil and heavy oil, and improving the uniformity of dilution. In addition, the slow flow rate of the well fluid on
the surface of the motor is not conducive to motor heat dissipation.
By installing a protective cover, the cross-sectional area of the well fluid flow can be reduced, the flow rate can be increased, and the
purpose of motor heat dissipation can be achieved.
Wide width electric pump is designed specifically for well conditions with large flow fluctuations. The impeller adopts a mixed phase
flow structure and optimizes the balance design of axial force. It can still operate normally and efficiently under conditions of large
liquid volume fluctuations.
Mixed flow design, with blade opening 30% wider than radial flow pump
A broader scope of work
Higher gas processing capability
Higher viscosity, scale, and sand adaptability
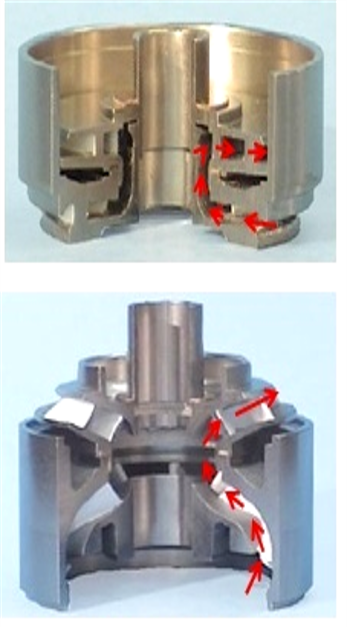
Technical characteristics:
The centrifugal pump adopts a compression structure to improve the wear resistance of the unit;
The design of a fully compressed structure combined with a high load-bearing protection device enables the unit to have a wider range of
displacement adaptability, and the flow rate can operate for extended periods of time within the recommended range;
The downward axial force of the impeller and pump shaft is borne by the high load protector, which reduces the wear of the impeller gasket
and improves the service life of the unit.
Applicable oil wells:
Oil wells with unclear production capacity;
Shale gas and coalbed methane extraction.
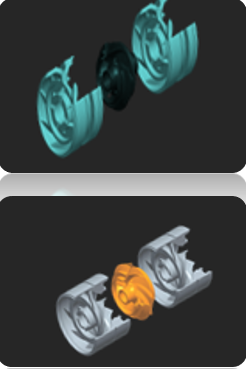
Conventional impeller 150m3/d
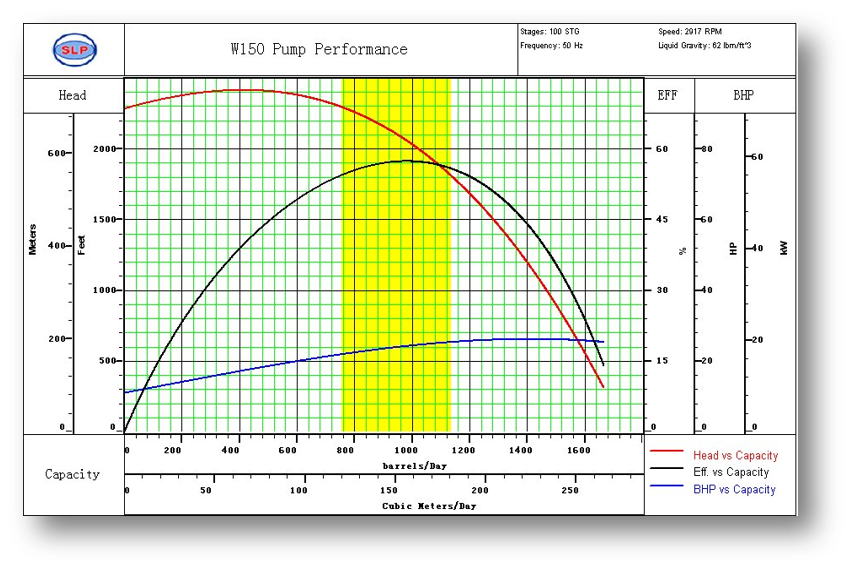
Wide guide impeller 150m3/d
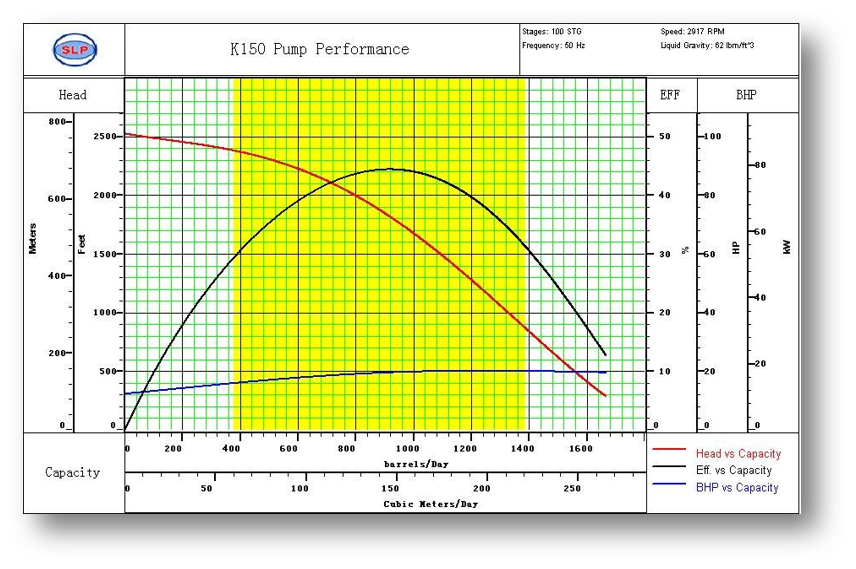
Small diameter electric pump unit configuration composition:
95 motor (89 permanent magnet motor);
86 capsule protector: two-stage capsule+sedimentation structure design;
86 separator: sand resistant liner, alloy bearing;
86 centrifugal pump: 30m3/d-300m3/d.
Unit projection size:
102mm(99mm)
Applicable oil wells:
1. Small diameter casing oil well;
2. Damaged oil wells;
3. Side drilling.
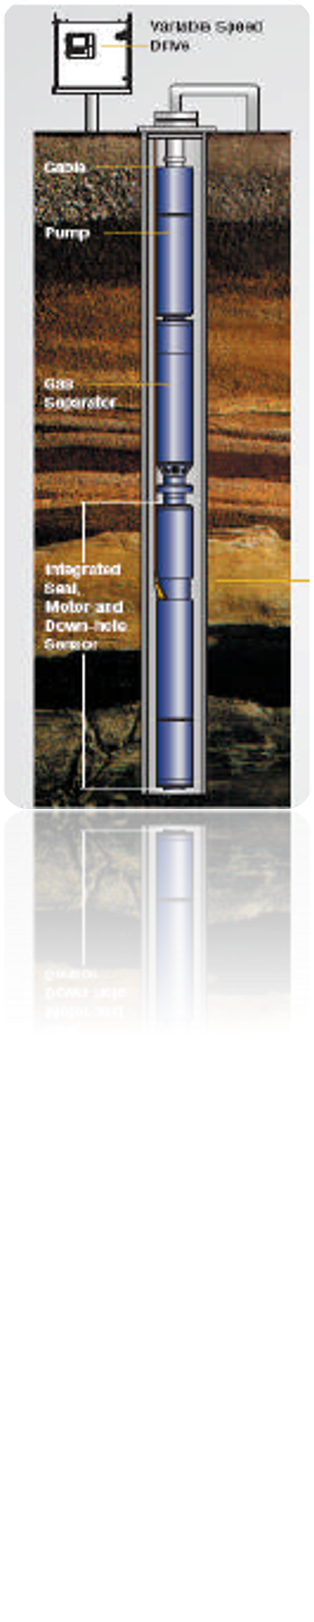
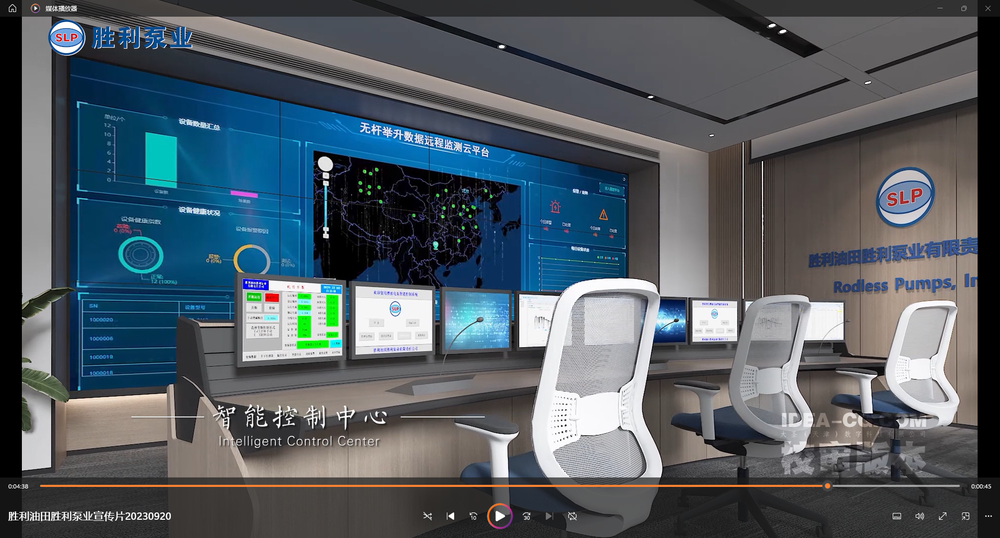
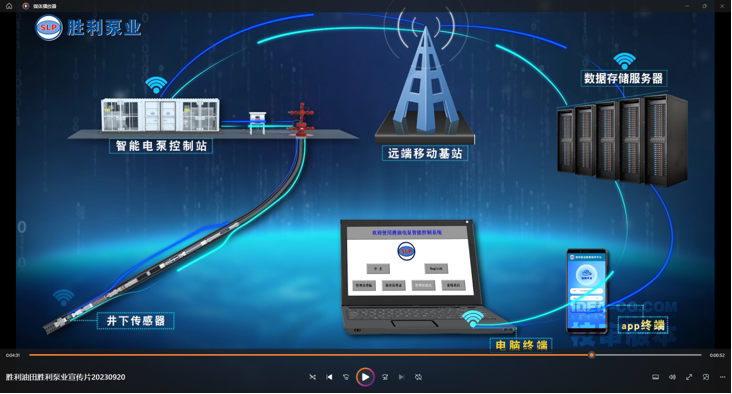
The intelligent control system for submersible electric pumps can self inspect and regulate the entire production process without manual intervention. The intelligent equipment has self inspection related functions, which can perfectly detect equipment problems through self inspection and evaluation and solve them in a timely manner. Five core technological advantages have been formed, including intelligent control technology, intelligent detection technology, intelligent diagnosis technology, intelligent prediction technology, and intelligent optimization technology. Through intelligence, more industry information can be obtained and applied on a large scale, reducing the overload work in electric pump management and implementing the simplest resource optimization and strengthened management.
|
|